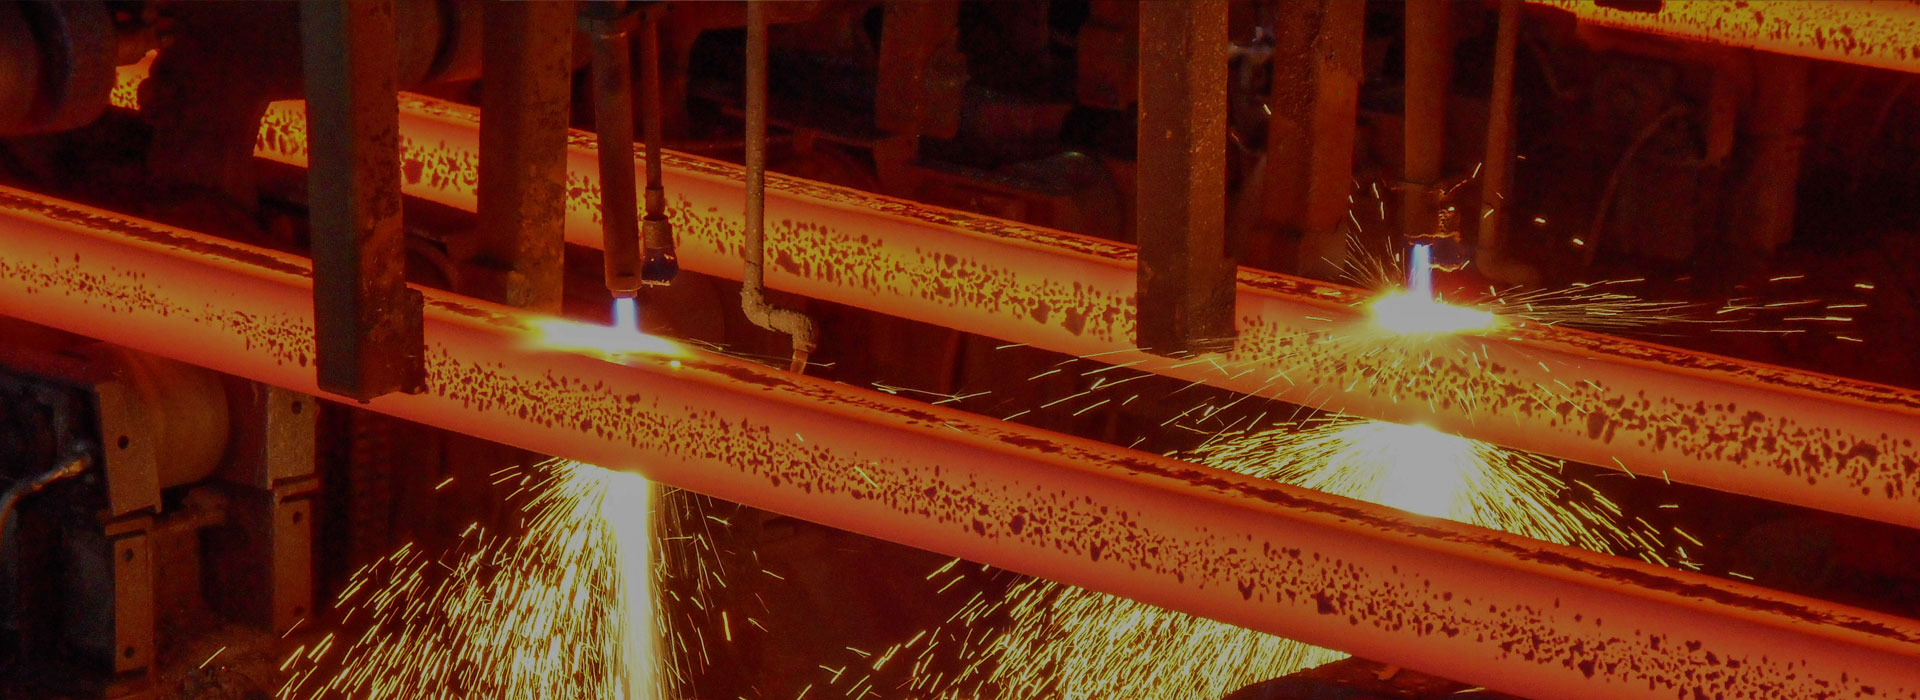
Inline inspection is often sold as a way to catch defects faster. On a real precision iron casting line, its bigger value is changing when decisions are made. I have worked with iron casting production at Ningbo Supreme Machinery Co., Ltd since the days when gray iron and ductile iron castings were inspected mostly by eye, tap, and caliper. The shift to automated lines and inline inspection has not removed the need for experience. It has moved that experience upstream—into melting, pouring, cooling, and even machining. This article looks at how inline inspection actually changes precision iron casting quality control, what technologies pay off, and where they still fall short.
Inline Inspection Is Not Just X-Ray: What We Actually Use on Iron Casting Lines
When customers hear that we use inline inspection for precision iron casting, many assume we are talking about X-ray every part. That is not realistic. X-ray is useful, but it is slow, expensive, and often overkill for a gray iron pump housing or a ductile iron valve body. What actually works on a production line is a layered approach: thermal analysis at the furnace, infrared monitoring at the pouring station, machine vision after cleaning, and targeted X-ray or ultrasonic testing for critical batches.
At Ningbo Supreme Machinery Co., Ltd, we have been producing iron casgrayntig, ductile iron casting, and precision investment casting for more than 25 years. The company started in 1990 with iron castings and stainless steel castings, then added a steel casting line after 2000. Over that time, our production lines have moved from manual working to automatic machinery. The one lesson that repeats is simple: inline inspection only works when it is tied to a process decision. If the data does not change the next heat, the next mold, or the next machining setup, it is just record-keeping.
The Cost Argument: Why a Rejected Casting Is Only the Visible Loss
When a precision iron casting is rejected at final inspection, the visible loss is the casting itself. The invisible loss is usually larger. You have already consumed melting energy, molding sand, labor, machining allowance, and sometimes a customer delivery slot. For a ductile iron hydraulic manifold made to ASTM A536 65-45-12, a shrinkage defect found after machining can mean a scrapped part that already has 2–3 mm of material removed from critical faces. That is not just a casting loss. It is a machining capacity loss.
This is why I prefer to judge inline inspection by how early it can intervene. A thermal analysis reading that flags a low residual magnesium trend before pouring can save an entire ladle. An infrared camera that catches a pouring temperature below 1380°C can prevent cold shuts in thin-wall gray iron castings. A machine vision station after shot blasting can catch a surface crack before the part reaches the machining center. None of these replace final inspection. They reduce the number of defects that ever reach final inspection.
Matching Inspection Technology to Gray Iron, Ductile Iron, and Investment Casting
Not every inline inspection technology fits every iron casting process. The table below is the practical comparison I use when configuring a line. It is not a theoretical ranking. It reflects what we have seen work on real production floors.
| Technology | Best Fit | Typical Detection Speed | Main Defects Caught | Limitation on Iron Casting |
|---|---|---|---|---|
| Thermal analysis | Melting and nodularization control | 30–90 seconds per heat | Carbon equivalent drift, nodularity fade, chill tendency | Indirect measurement; needs calibration with metallography |
| Infrared thermal imaging | Pouring temperature and mold filling | Real time during pour | Cold shuts, misruns, pouring temperature deviation | Line-of-sight only; smoke and ladle positioning can interfere |
| Machine vision | Surface inspection after cleaning | 1–5 seconds per part | Cracks, burrs, cold shuts, missing material, sand inclusion | Cannot see internal defects; lighting and part orientation matter |
| Real-time X-ray | Safety-critical ductile iron and steel castings | 10–60 seconds per part | Shrinkage porosity, internal cracks, inclusions | High cost; slower line speed; radiation safety requirements |
| Ultrasonic testing | Heavy-section ductile iron and steel castings | 2–10 seconds per point | Internal voids, cracks, nodularity variation in thick sections | Requires coupling; complex geometries are difficult |
For gray iron castings such as hydraulic valve bodies and machine tool components, machine vision and infrared pouring monitoring usually deliver the best return. Gray iron's flake graphite gives it good damping and thermal conductivity, but it also means surface defects are common enough to justify automated visual inspection. For ductile iron castings, thermal analysis and targeted X-ray matter more because nodularity and internal soundness directly affect elongation and fatigue life. For precision investment casting, the priority shifts to wax pattern dimensions and shell integrity, where laser scanning and process data logging often matter more than inline radiography.
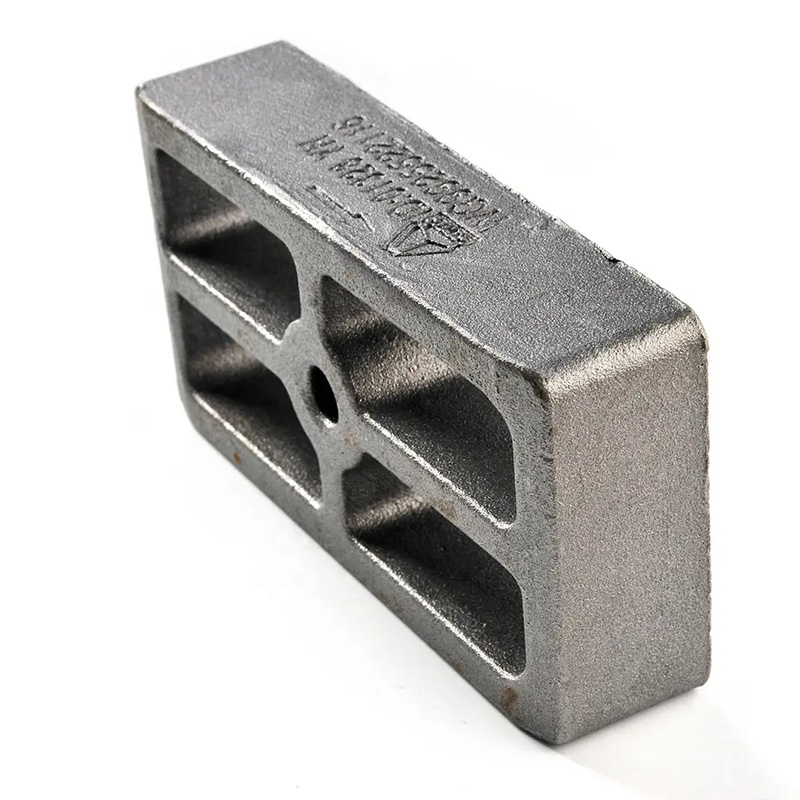
How Inline Inspection Connects to Machining and Assembly
One thing I have learned from years of producing iron castings at Ningbo Supreme Machinery Co., Ltd is that quality control cannot stop at the foundry door. A precision iron casting that passes dimensional inspection can still fail at the machining center if the casting's hardness or microstructure varies. Gray iron with chill, for example, can measure within tolerance but destroy carbide tooling. Ductile iron with low nodularity can machine easily but fail a pressure test.
This is where inline inspection data becomes valuable beyond the foundry. When we record thermal analysis results, pouring temperatures, and cooling data by batch, we can correlate them with machining performance. If a customer reports chatter or excessive tool wear on a specific batch of gray iron castings, we can trace back to the carbon equivalent and cooling rate. If a ductile iron casting fails a leak test after machining, we can review the magnesium residual and nodularity trend. That traceability is not glamorous, but it is what turns quality control into process control.
For customers who receive both iron castings and finished machined parts from us, this linkage reduces the blame game. Instead of arguing whether the defect came from casting or machining, we can look at the data together.
A Practical Configuration Example for Ductile Iron Hydraulic Manifolds
Let me give a concrete example. Suppose we are running a ductile iron hydraulic manifold with a wall thickness of 8–12 mm, material ASTM A536 65-45-12, and a machining allowance of 2.5 mm on critical faces. The customer requires a pressure tightness test after machining and a nodularity of at least 85%.
On the melting side, we would use optical emission spectrometry for chemistry and thermal analysis for carbon equivalent and nodularity trend. The target window is C 3.5–3.7%, Si 2.2–2.5%, Mg 0.04–0.06%. On the pouring side, infrared thermal imaging monitors the pouring temperature, keeping it between 1390°C and 1420°C. After cleaning, machine vision checks for surface cracks and cold shuts. For critical batches, real-time X-ray or ultrasonic testing checks internal shrinkage in the thick section around the port bosses.
This configuration does not inspect every part with X-ray. It uses the right technology at the right stage. The result is fewer surprises at machining and a more stable pressure test pass rate. In my experience, that combination matters more than buying the most expensive inspection machine on the market.
What I Would Check Before Buying an Inline Inspection System
If you are evaluating inline inspection for precision iron casting, I would ask four questions before looking at equipment brochures. First, what defect are you trying to prevent, and at what process stage does it originate? Second, what will you do with the data—will it change a setpoint, stop a pour, or adjust a machining offset? Third, what is the cost of a missed defect versus the cost of the inspection system? Fourth, who will maintain and calibrate the system after installation?
At Ningbo Supreme Machinery Co., Ltd, our production has evolved from manual working to automatic machinery because automation solves consistency problems that manual work cannot. But automation without process feedback is just faster variation. Inline inspection is the feedback loop that makes automation useful for precision iron casting quality control.
Frequently Asked Questions
Does inline inspection replace final inspection for iron castings?
No. Inline inspection reduces the number of defects that reach final inspection, but final inspection is still necessary for batch sampling and customer-specific acceptance criteria. For safety-critical ductile iron castings, final dimensional and pressure testing remains mandatory.
Which inline inspection technology is most cost-effective for gray iron casting?
For most gray iron casting lines, machine vision after cleaning and infrared pouring temperature monitoring offer the fastest payback. They catch surface defects and cold shuts without slowing the line significantly. Thermal analysis is also important, but it is a melting control tool rather than a part inspection tool.
Can inline inspection detect nodularity problems in ductile iron before pouring?
It can indicate a trend, but it does not give a final nodularity number in real time. Thermal analysis combined with rapid metallography can show whether the magnesium residual and cooling curve are within the expected window. If the trend is outside the window, the foundry can adjust the treatment or pouring sequence.
How does Ningbo Supreme Machinery Co., Ltd support inline inspection for investment casting?
For precision investment casting, we focus on wax pattern dimensional stability, shell thickness, and pouring temperature records. Laser scanning and process data logging are often more useful than inline X-ray for these castings. We configure the inspection approach based on the alloy, geometry, and customer acceptance standard.
What standards are commonly referenced for iron casting inspection?
Common references include ASTM A48 for gray iron, ASTM A536 for ductile iron, ISO 1083 for spheroidal graphite cast irons, ISO 8062 for dimensional tolerances, and ASTM E446 or E186 for radiographic examination. The applicable standard depends on the material and application.
If you are evaluating inline inspection for a precision iron casting project, or want to discuss gray iron, ductile iron, or investment casting quality control, you can contact Ningbo Supreme Machinery Co., Ltd directly. Share your material grade, critical dimensions, and defect concerns, and we can help define a practical inspection configuration for your production line.